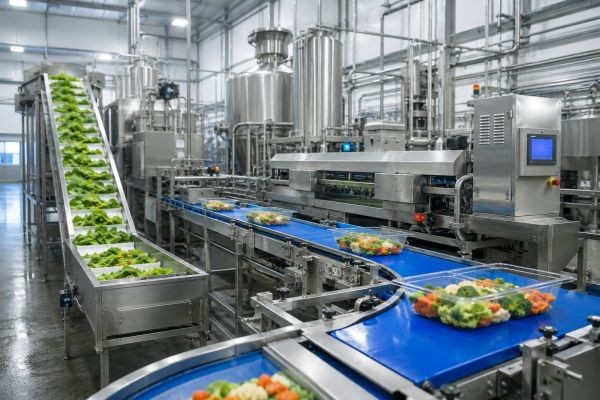
Modern food manufacturing depends on reliable equipment that delivers consistent production, maintains product quality, and supports food safety throughout every stage of processing. Whether producing dairy products, beverages, bakery items, snacks, frozen foods, or packaged meals, selecting suitable machinery plays a major role in improving operational efficiency and reducing production costs. Investing in equipment without evaluating production requirements can lead to unnecessary downtime, higher maintenance expenses, and inconsistent product quality.
Every food manufacturing facility has unique production goals based on product type, processing methods, production volume, hygiene requirements, and regulatory standards. Because manufacturing conditions vary from one facility to another, equipment selection should always begin with a detailed assessment of operational needs. Careful planning allows manufacturers to improve productivity while supporting long-term business growth.
Many manufacturers evaluate different types of food processing machinery [https://mekantratech.com/food-beverage-processing-machinery/]by comparing production capacity, hygienic design, automation capabilities, material compatibility, maintenance requirements, and operating efficiency. Understanding these factors helps decision-makers invest in equipment that delivers reliable performance while meeting food production objectives.
Selecting industrial equipment should focus on long-term operational value instead of purchase price alone. Durable machinery with efficient performance, lower operating costs, and simplified maintenance often provides greater financial returns while supporting consistent production over many years.
Understand Production Requirements
Every successful equipment selection process begins with clearly defining production objectives.
Before comparing equipment options, manufacturers should evaluate:
- Daily production targets
- Product characteristics
- Ingredient properties
- Processing temperatures
- Production schedules
- Packaging requirements
- Hygiene standards
- Future expansion plans
Clearly understanding these requirements helps narrow equipment choices while improving purchasing decisions.
Prioritize Food Safety
Food safety remains one of the most important considerations when selecting manufacturing equipment.
Reliable systems should support:
- Hygienic production
- Easy cleaning
- Contamination prevention
- Safe material handling
- Regulatory compliance
- Product consistency
Equipment designed with food safety in mind helps manufacturers maintain product quality while protecting consumers.
Evaluate Material Selection
Construction materials directly affect equipment durability and food safety.
Manufacturers commonly select materials that provide:
- Corrosion resistance
- Easy cleaning
- Long service life
- Chemical resistance
- Smooth product contact surfaces
High-quality construction materials reduce contamination risks while improving equipment reliability.
Determine Production Capacity
Equipment capacity should align with both current production demands and future growth plans.
Important factors include:
- Batch size
- Continuous production requirements
- Daily output
- Peak production periods
- Future capacity expansion
Selecting equipment with appropriate capacity helps improve efficiency without creating unnecessary operating costs.
Consider Process Requirements
Different food products require different processing methods.
Common manufacturing operations include:
- Mixing
- Heating
- Cooling
- Blending
- Homogenizing
- Filling
- Packaging
- Storage
Understanding the complete production process ensures selected equipment integrates smoothly into manufacturing operations.
Focus on Energy Efficiency
Energy costs significantly influence long-term production expenses.
Modern equipment often includes technologies that improve efficiency while maintaining stable production performance.
Benefits include:
- Lower operating costs
- Reduced energy consumption
- Better process control
- Improved production consistency
- Environmental benefits
Energy-efficient equipment often delivers greater long-term value despite higher initial investment costs.
Evaluate Automation Features
Automation continues transforming food manufacturing by improving consistency and reducing manual intervention.
Useful automation features include:
- Digital monitoring
- Automated process control
- Performance reporting
- Remote monitoring
- Alarm systems
- Production data collection
Automation helps manufacturers improve productivity while maintaining stable operating conditions.
Review Cleaning Requirements
Frequent cleaning is necessary in food production environments.
Before selecting equipment, evaluate:
- Cleaning accessibility
- Surface design
- Component removal
- Cleaning frequency
- Sanitation procedures
Equipment designed for easy cleaning reduces downtime while supporting food safety requirements.
Assess Maintenance Requirements
Routine maintenance directly affects production reliability.
Review maintenance considerations such as:
- Inspection schedules
- Spare parts availability
- Lubrication requirements
- Service accessibility
- Replacement components
Equipment requiring simple maintenance procedures often improves long-term operational efficiency.
Evaluate Equipment Reliability
Reliable machinery contributes to uninterrupted production and consistent product quality.
Key reliability factors include:
- Manufacturing quality
- Component durability
- Operating performance
- Service support
- Equipment lifespan
- Proven industry experience
Reliable equipment reduces production interruptions while improving manufacturing efficiency.
Plan for Future Growth
Successful food manufacturers often expand production as market demand increases.
Future planning should consider:
- Higher production volumes
- Additional product lines
- Expanded facilities
- Automation upgrades
- New processing technologies
Selecting scalable equipment today reduces future replacement costs while supporting long-term business development.
Consider Environmental Sustainability
Modern food manufacturers are placing greater emphasis on environmentally responsible production practices. Selecting equipment that supports efficient resource management can reduce operating costs while helping facilities meet sustainability goals.
Important environmental factors include:
- Energy efficiency
- Water conservation
- Waste reduction
- Emission control
- Recyclable materials
- Noise reduction
Environmentally friendly equipment contributes to responsible manufacturing while improving long-term operational performance.
Analyze Total Operating Costs
The purchase price of machinery represents only a portion of the overall investment. Daily operating expenses often determine the true cost of ownership over the equipment's service life.
Evaluate expenses related to:
- Energy usage
- Maintenance
- Spare parts
- Cleaning supplies
- Operator training
- Production downtime
Choosing machinery with lower operating costs often provides greater value over many years.
Select a Reliable Equipment Supplier
The performance of manufacturing equipment is closely linked to the quality of the supplier.
Before making a purchasing decision, review:
- Industry experience
- Manufacturing standards
- Product quality
- Technical support
- Installation assistance
- After-sales service
A dependable supplier helps ensure reliable equipment performance and long-term operational support.
Train Equipment Operators
Well-trained operators play an important role in maintaining safe and efficient production.
Training should include:
- Equipment operation
- Safety procedures
- Cleaning methods
- Routine inspections
- Basic troubleshooting
- Emergency response
Proper training minimizes operational errors while extending equipment life.
Monitor Equipment Performance
Routine performance monitoring helps manufacturers detect potential issues before they interrupt production.
Important performance indicators include:
- Production output
- Equipment availability
- Energy consumption
- Product consistency
- Maintenance frequency
- Operating efficiency
Monitoring these indicators supports continuous process improvement and better equipment management.
Schedule Preventive Maintenance
Preventive maintenance helps reduce unexpected breakdowns that may interrupt production schedules.
A structured maintenance program should include:
- Routine inspections
- Lubrication
- Calibration
- Component replacement
- Safety testing
- Cleaning verification
Regular maintenance extends equipment life while improving production reliability.
Evaluate Return on Investment
Manufacturing equipment should generate long-term value rather than only meeting immediate production requirements.
Factors affecting return on investment include:
- Increased productivity
- Lower maintenance costs
- Reduced operating expenses
- Better product quality
- Longer equipment lifespan
- Improved production capacity
Evaluating these benefits helps manufacturers make informed investment decisions.
Common Equipment Selection Mistakes
Many manufacturers experience operational problems because equipment is selected without thorough evaluation.
Common mistakes include:
- Choosing equipment based only on purchase price
- Ignoring hygiene requirements
- Selecting incorrect production capacity
- Overlooking maintenance needs
- Underestimating future expansion
- Failing to assess supplier support
Avoiding these mistakes helps improve production efficiency and reduces costly operational disruptions.
Build a Long-Term Equipment Strategy
Equipment selection should support long-term manufacturing goals rather than short-term production demands.
An effective strategy includes:
- Production planning
- Equipment evaluation
- Preventive maintenance
- Staff training
- Process monitoring
- Continuous improvement
Combining these practices creates a reliable manufacturing environment that supports consistent product quality and sustainable business growth.
Final Thoughts
Choosing the right machinery for modern food manufacturing plants requires careful planning, technical evaluation, and a long-term perspective. Manufacturers should consider production requirements, hygiene standards, automation capabilities, energy efficiency, maintenance needs, equipment reliability, and supplier support before making an investment. Looking beyond the initial purchase price allows businesses to select machinery that delivers dependable performance, lower operating costs, and greater production flexibility. A structured equipment selection process helps improve productivity, maintain food safety, reduce downtime, and support long-term manufacturing success.
Frequently Asked Questions
What should manufacturers consider before purchasing food manufacturing equipment?
Manufacturers should evaluate production capacity, hygiene standards, material compatibility, energy efficiency, maintenance requirements, automation features, and future production plans before selecting equipment.
Why is hygienic equipment important in food manufacturing?
Hygienic equipment helps prevent contamination, supports food safety regulations, simplifies cleaning, and maintains consistent product quality throughout the production process.
How does preventive maintenance benefit food processing equipment?
Preventive maintenance reduces unexpected breakdowns, extends equipment lifespan, improves operational reliability, and helps maintain continuous production.
Why should manufacturers evaluate total operating costs instead of purchase price?
Long-term expenses such as energy, maintenance, spare parts, and downtime often have a greater financial impact than the equipment's initial purchase cost.
How can automation improve food manufacturing operations?
Automation improves production consistency, reduces manual errors, supports performance monitoring, increases efficiency, and helps manufacturers maintain stable processing conditions.


